From Molecule to Manufacturing
A disciplined, six-stage process and a robust production infrastructure keep every API consistent, compliant and ready for global markets.
Raw Material Sourcing
Qualified vendors and raw material QC testing ensure every input meets specification.
Process R&D & Route Optimization
Synthesis routes are refined for yield, purity and cost before commercial scale-up.
Pilot Scale-Up & Validation
Lab-scale processes are validated at pilot scale to confirm consistency.
GMP Commercial Manufacturing
Production runs in GMP-certified reactors under strict in-process controls.
QC / QA Release Testing
Every batch is tested against validated methods and released only after QA sign-off.
Packaging & Global Dispatch
Compliant packaging and documentation prepare each shipment for export markets.
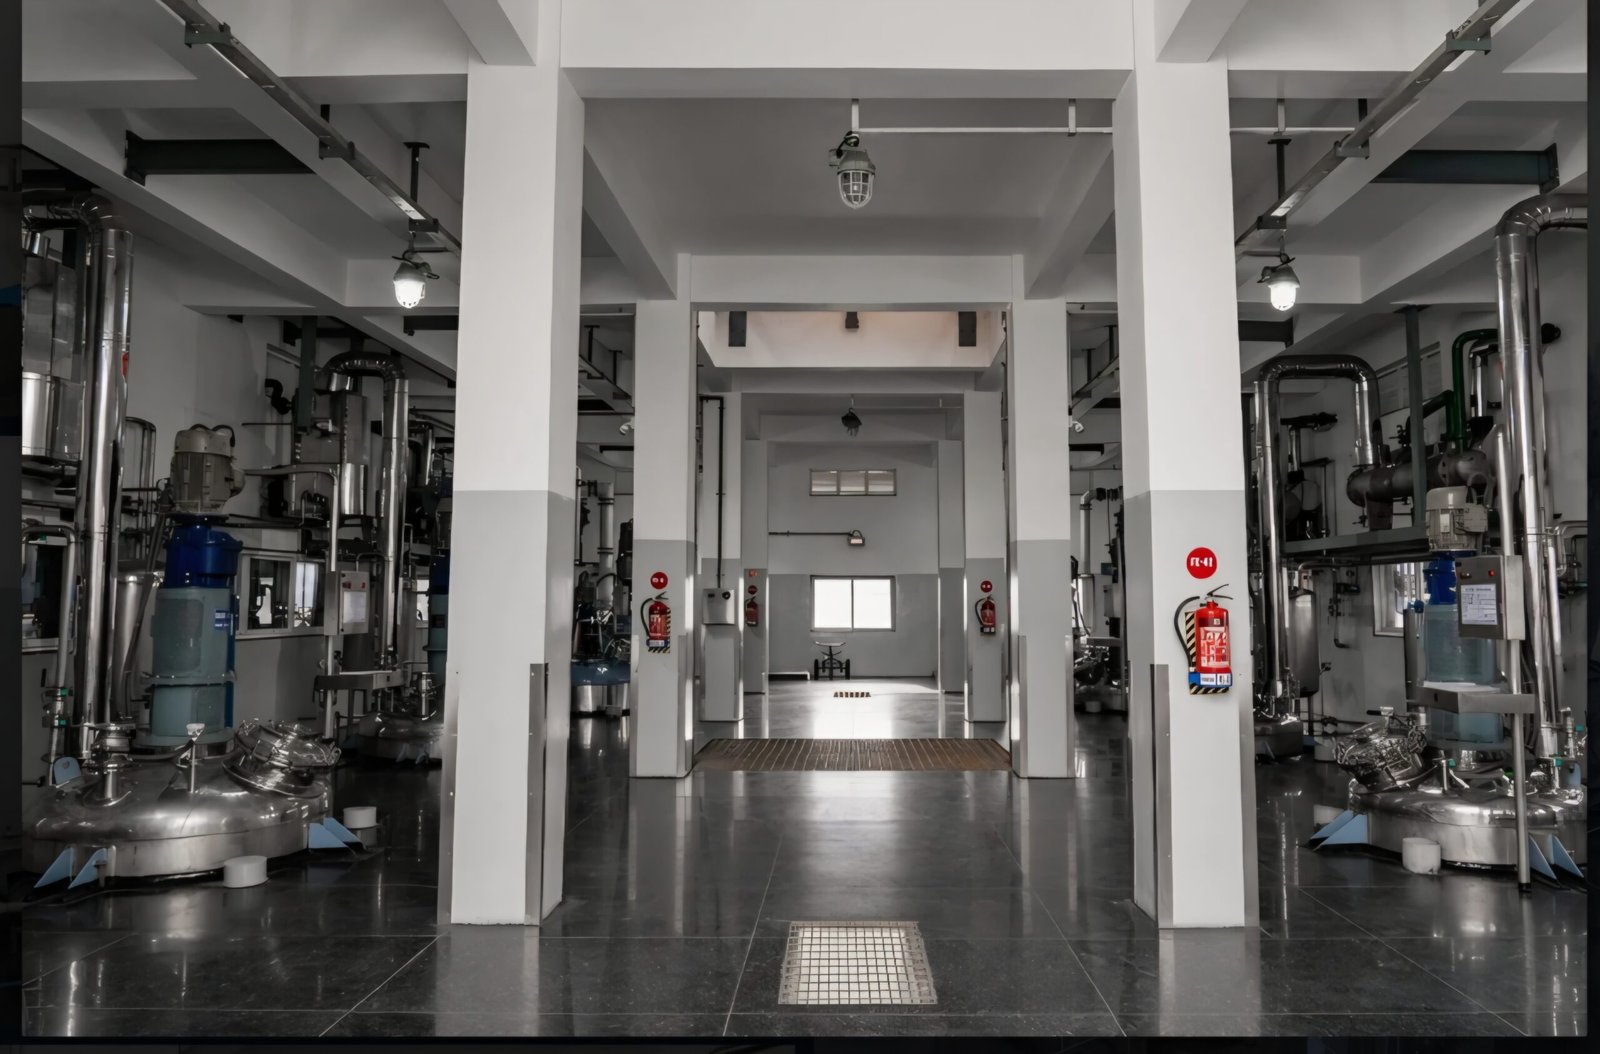
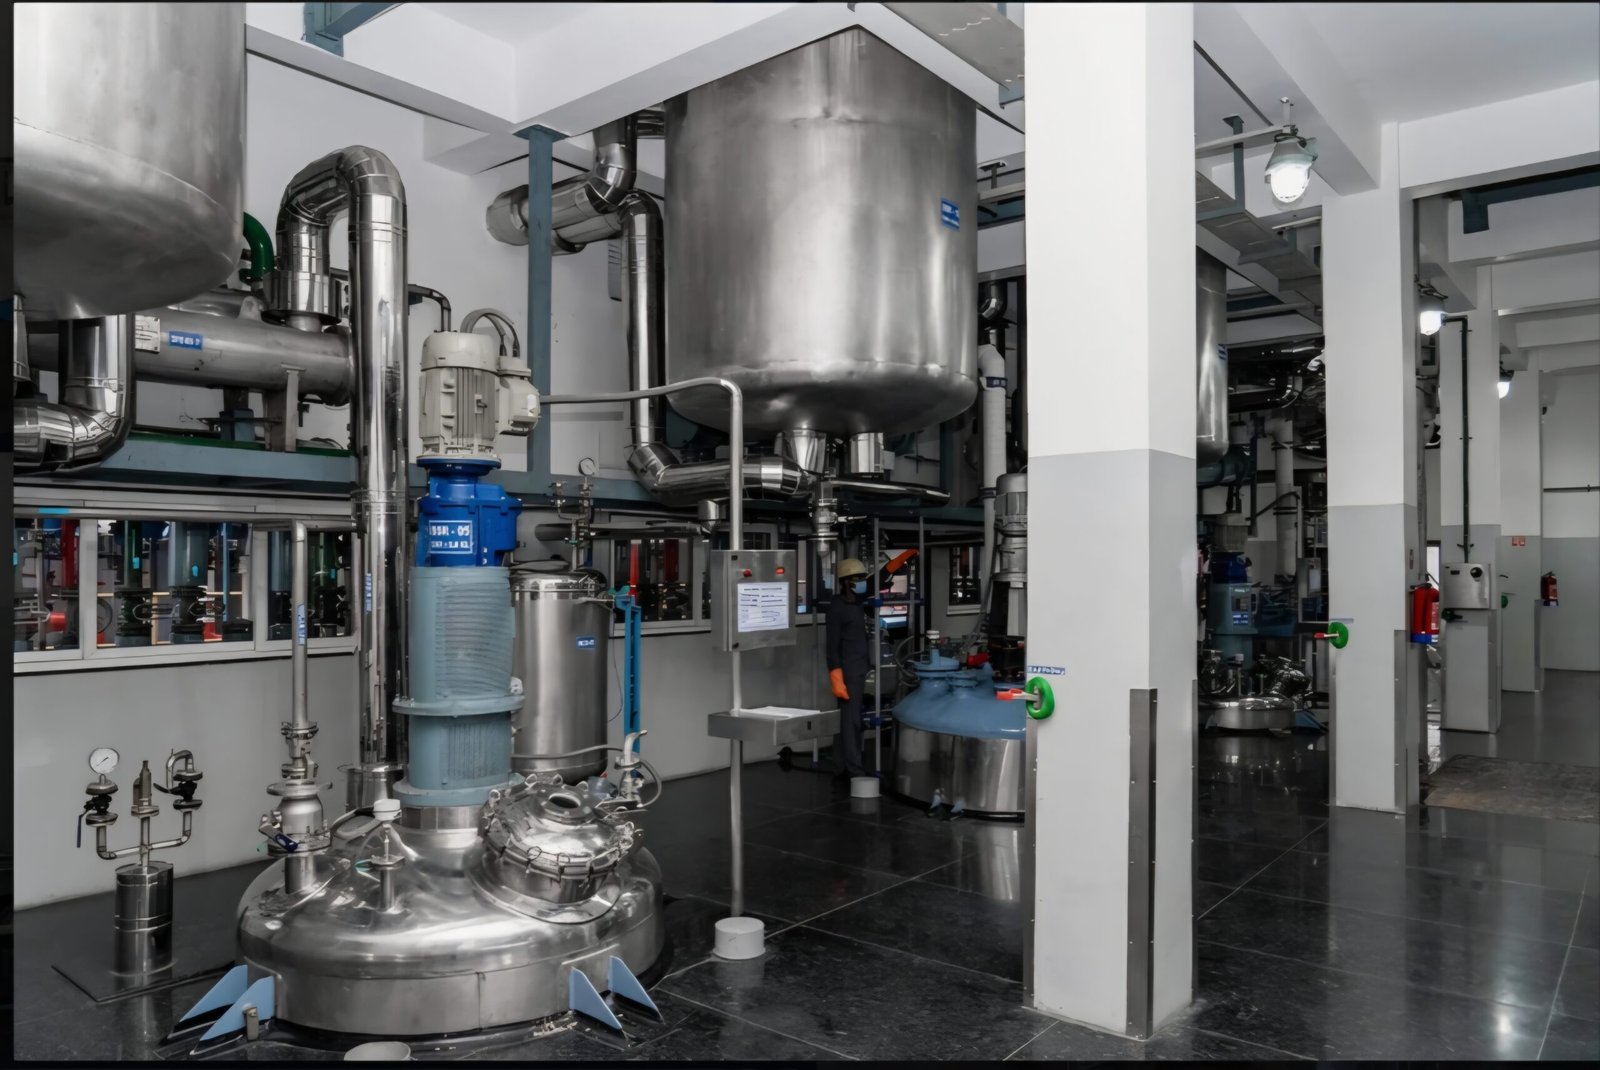
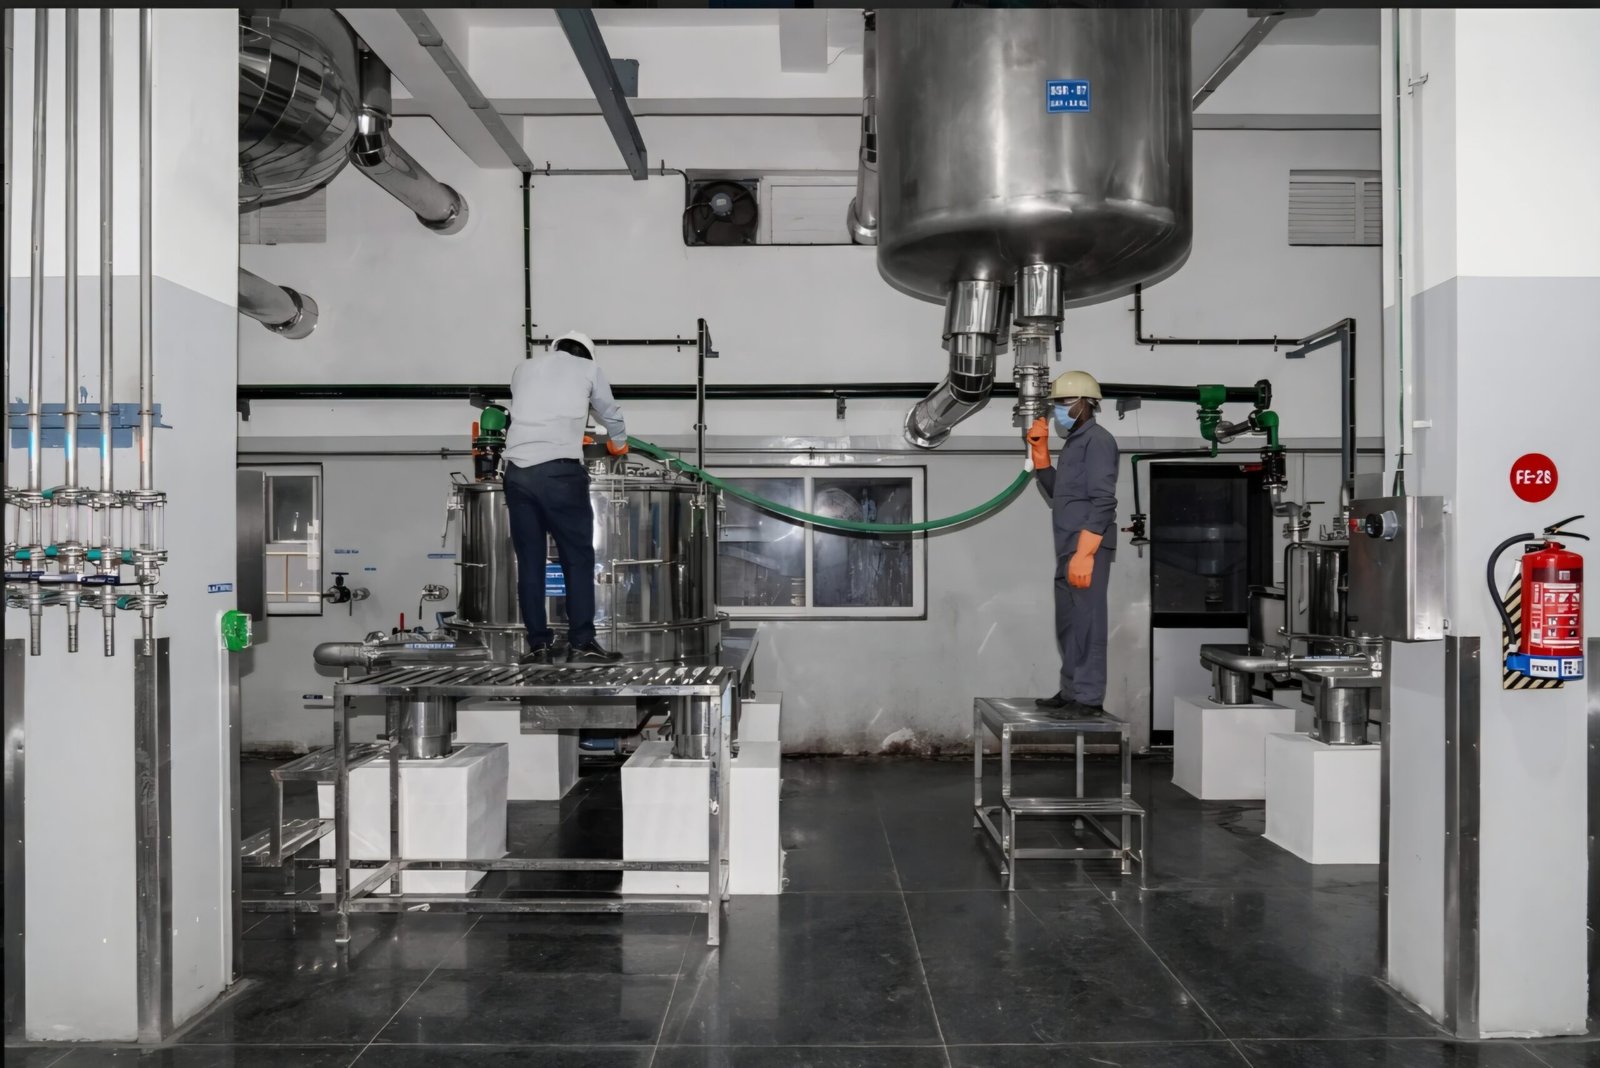
Built for Scale, Engineered for Consistency
Modern facilities, redundant utilities and dedicated production blocks keep manufacturing running around the clock — without compromising on quality.
Inside Our Production Plant
Looking to Partner With Our Manufacturing Team?
Talk to us about capacity, timelines and technical requirements for your next API.
Get In Touch